Explosive and munition manufacturing demands precise humidity control. Moisture levels in these facilities directly impact safety, product integrity, and regulatory compliance. Even small deviations from target relative humidity (RH) can trigger chemical degradation, static discharge events, or dimensional instability in pressed charges.
Facilities handling propellants, primers, and energetic materials must maintain zone-specific RH ranges throughout production, storage, and assembly. The consequences of failure range from batch rejection to catastrophic safety incidents.
Why Humidity Control Is Critical in Explosive Manufacturing
Uncontrolled moisture creates compounding hazards across every production stage. Each area requires specific humidity parameters to prevent chemical reactions, physical changes, and safety incidents.
Primary Moisture-Related Hazards
- Chemical degradation of propellants leading to unpredictable burn rates
- Powder caking that disrupts automated dosing systems
- Primer and fuse corrosion reducing ignition reliability
- Static electricity buildup from low humidity (below 40% RH)
- Dimensional instability in pressed charges affecting ballistic performance
- Moisture migration causing hot spots in stored materials
These risks multiply when facilities handle multiple explosive types with different moisture sensitivities. Modern munition plants must maintain precise environmental conditions across diverse production zones, from raw material storage through final assembly.
Static Discharge Prevention Through Humidity
Electrostatic discharge (ESD) is one of the most dangerous ignition sources in explosive manufacturing. Maintaining RH between 45% and 55% allows moisture in the air to increase surface conductivity, helping static charges dissipate before reaching dangerous levels.
Below 40% RH, charge accumulation accelerates rapidly. Dry air acts as an insulator, allowing static to build on equipment surfaces, personnel, and the explosive materials themselves. The IECEx framework for hazardous area classification identifies ESD as a primary ignition risk in Zone 1 and Zone 2 environments.
Higher RH also promotes particle agglomeration, reducing airborne dust concentrations. Fine explosive dust suspended in air presents both an inhalation hazard and a secondary explosion risk, making humidity-assisted dust suppression a valuable layer of protection.
Zone-Specific Humidity Requirements
Different areas within explosive manufacturing facilities require distinct humidity ranges based on the materials handled and processes performed. Maintaining these parameters prevents both immediate safety hazards and long-term product degradation.
| Production Zone | Target RH Range | Primary Control Objective |
|---|---|---|
| Raw Material Storage | 20–30% | Prevent hygroscopic absorption |
| Powder Processing | 25–35% | Minimise static generation |
| Mixing Operations | 30–35% | Maintain flow characteristics |
| Pressing/Loading | 35–40% | Ensure consistent density |
| Assembly Areas | 35–45% | Balance static control with corrosion prevention |
| Quality Testing | 40–50% | Standardise test conditions |
| Finished Storage | 25–35% | Maximise shelf life |
For areas where sealed containers of HMX or polyurethane-based propellants are opened, a tighter target of 40% ±10% RH is standard practice to prevent moisture absorption that alters burn characteristics.
Transitioning materials between zones with different humidity levels requires careful staging to prevent condensation or rapid moisture loss.
ATEX and IECEx Compliance for Equipment
Explosive manufacturing environments demand humidity control equipment that meets strict hazardous-area certifications. In Australia, equipment must comply with AS/NZS 60079 (the local adoption of IEC 60079) and align with the ATEX directives 2014/34/EU (equipment) and 1999/92/EC (workplace safety).
Zone Classification and Equipment Requirements
Hazardous areas are classified by the likelihood and duration of explosive atmospheres:
- Zone 0 / Zone 20 (gas/dust): Explosive atmosphere present continuously or for long periods
- Zone 1 / Zone 21: Likely to occur during normal operations
- Zone 2 / Zone 22: Not likely during normal operations, only briefly
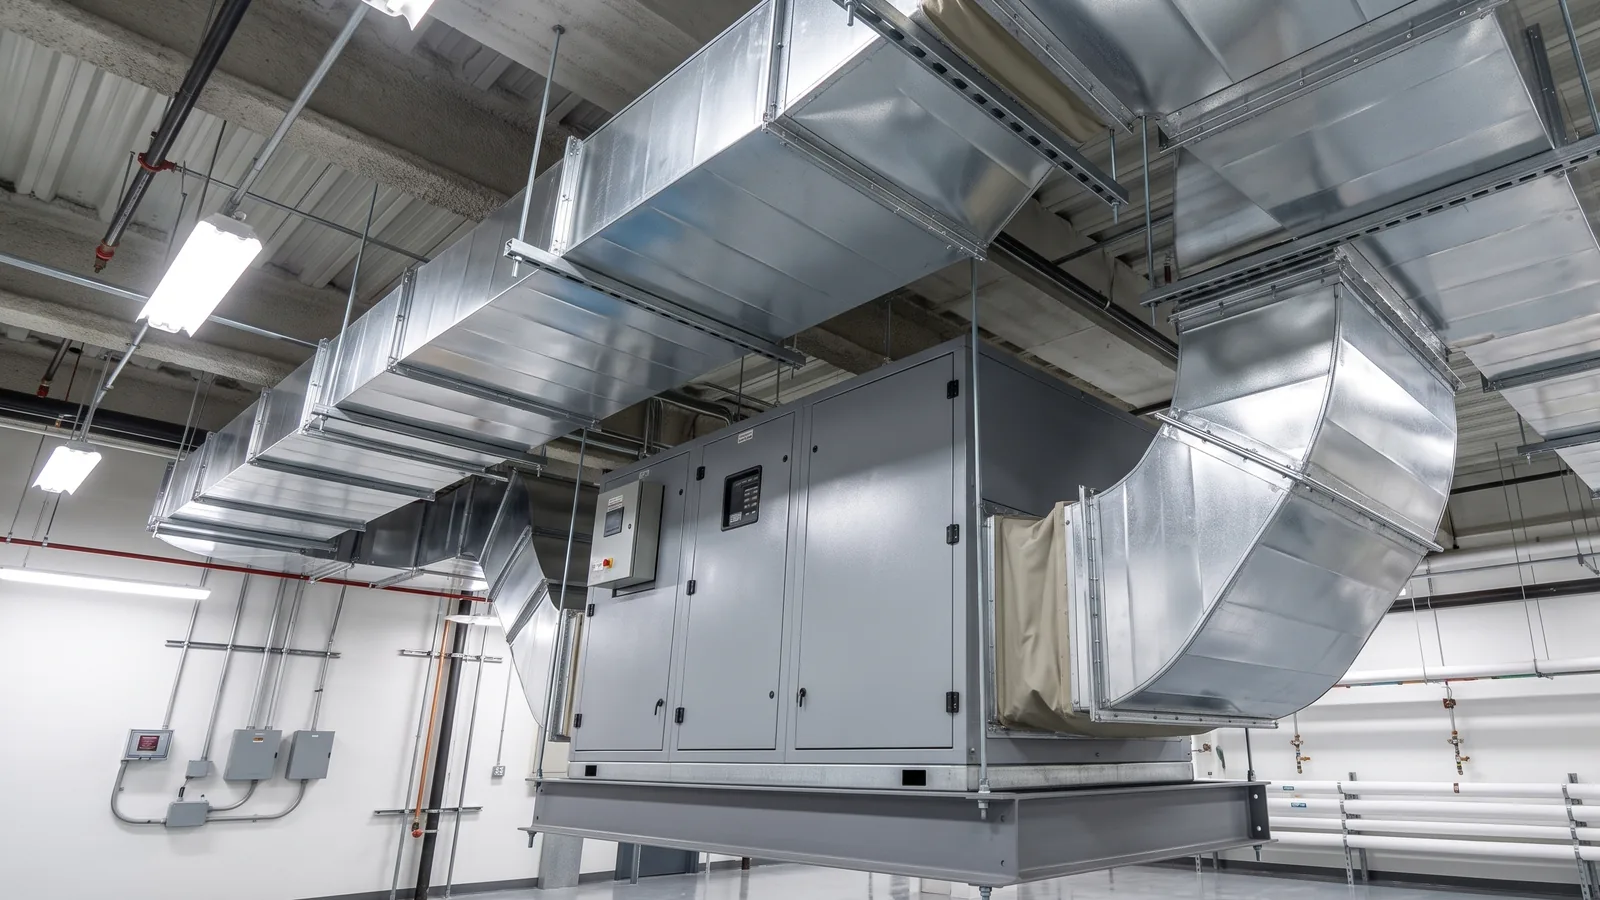
All humidity control equipment in these zones must feature explosion-proof motors, intrinsically safe control systems, spark-resistant construction, and fail-safe operation modes. Ducted dehumidification systems allow centralised equipment placement outside hazardous zones while distributing conditioned air throughout the facility, reducing the certification burden.
Essential Safety Features
- ATEX or IECEx certification appropriate to the zone classification
- Explosion-proof motors and electrical enclosures
- Intrinsically safe sensors and control wiring
- Spark-resistant and antistatic construction materials
- Fail-safe shutdown preventing unsafe humidity excursions
- Remote monitoring capability for restricted-access areas
Process-Specific Humidity Challenges
Each stage of explosive manufacturing presents unique moisture control requirements that directly impact product safety and performance.
Nitration and Chemical Processing
Nitration reactions generate significant heat and water vapour, requiring rapid moisture removal to prevent runaway reactions. Humidity spikes during these processes can cause premature reactions or product decomposition. Desiccant dehumidifiers used in pharmaceutical clean rooms apply the same rapid-response moisture removal principles needed here.
Powder Blending and Granulation
Explosive powders exhibit extreme sensitivity to moisture content, with even minor variations affecting flow properties and packing density. Consistent low humidity prevents clumping while maintaining safe static discharge conditions similar to electronics manufacturing.
Pressing and Consolidation
Moisture content directly influences the compressibility of explosive materials and the mechanical strength of pressed charges. Propellants, binders, and polymer components change dimensionally with humidity shifts, and uncontrolled RH during pressing creates density inconsistencies that affect detonation characteristics.
Monitoring, Traceability, and Control Integration
Regulatory frameworks require continuous environmental recording so that the conditions under which each batch was produced can be traced and verified. Thermohygrographs and digital data loggers record temperature and humidity throughout production cycles, providing an audit trail if a defect is identified post-manufacture.
Key Monitoring Parameters
- Real-time humidity mapping across production zones
- Dewpoint tracking to prevent condensation during zone transitions
- Temperature-humidity correlation analysis
- Airflow patterns affecting moisture distribution
- Equipment performance metrics and fault detection
- Historical trending for process optimisation
Integration between humidity control systems and building management systems (BMS) enables automated response to environmental changes. Facilities using BMS-connected industrial dehumidifiers can trigger alarms, adjust setpoints, and log excursions without manual intervention.
Selecting Dehumidification Technology
The choice between refrigerant and desiccant dehumidification depends on target humidity levels, ambient temperatures, and process requirements. Explosive manufacturing frequently requires ultra-low RH levels that favour desiccant technology.
Desiccant dehumidifiers excel at achieving the 20–35% RH ranges common in powder storage and processing areas. YAKE desiccant units operate from -20°C to +50°C, maintaining full performance in cold magazines and unheated storage buildings where refrigerant dehumidifiers fail below 15°C.
Technology Selection Criteria
- Required humidity range and allowable tolerance
- Ambient temperature range (cold magazines vs heated production areas)
- Air volume and recirculation requirements
- Energy efficiency at design conditions
- Maintenance accessibility in restricted-access zones
- N+1 redundancy requirements for safety-critical processes
Implementation Best Practices
Successful humidity control in explosive manufacturing requires careful planning from design through ongoing operations. Facilities must balance safety requirements with operational efficiency while maintaining strict environmental parameters.
Design Considerations
- Segregation of humidity zones with airlocks and staged transitions
- Redundant systems for safety-critical areas
- Service access points located outside hazardous zones
- Backup power systems for continuous operation during outages
- Gradual humidity transitions to prevent condensation on materials
- Integration with explosion suppression and ventilation systems
Regular validation of system performance ensures continued compliance with both safety standards and quality requirements. Preventive maintenance schedules must account for the unique challenges of servicing equipment in hazardous environments, including lockout/tagout procedures and desiccant dehumidifier service intervals.
Frequently Asked Questions
What humidity level prevents static discharge in explosive manufacturing?
Maintaining relative humidity between 45% and 55% allows moisture on surfaces and in the air to dissipate electrostatic charges before they reach ignition energy levels. Below 40% RH, static accumulation accelerates significantly.
Do explosive manufacturing facilities need ATEX-certified dehumidifiers?
Any humidity control equipment operating within a classified hazardous zone (Zone 0, 1, or 2 for gases; Zone 20, 21, or 22 for dusts) must carry ATEX or IECEx certification. Ducted systems placed outside the hazardous zone only need certification on components inside the zone boundary.
Why are desiccant dehumidifiers preferred for munition storage?
Cold magazines and unheated storage areas often drop below 15°C, where refrigerant dehumidifiers lose effectiveness. Desiccant units maintain full moisture removal capacity from -20°C to +50°C, making them the standard choice for munition storage environments.
How is humidity monitored for regulatory compliance in explosive production?
Facilities use calibrated thermohygrographs and digital data loggers to create a continuous environmental record. This traceability allows investigators to verify the production conditions for any batch if a defect or incident is identified post-manufacture.
What happens if humidity is too high during propellant pressing?
Excess moisture alters the compressibility of explosive materials and causes dimensional changes in binders and polymer components. The result is density inconsistencies in pressed charges, which directly affect burn rates and detonation characteristics.
Talk to Moisture Cure Commercial
Moisture Cure Commercial has supplied dehumidifiers and humidifiers to Australian businesses for over 20 years. Whether you need help selecting the right unit for a hazardous-area application, sizing a system for your facility, or troubleshooting an existing setup, our team can help.
Call us on (02) 6584 2511 or contact us online to discuss humidity control for your explosive or munition manufacturing operation.