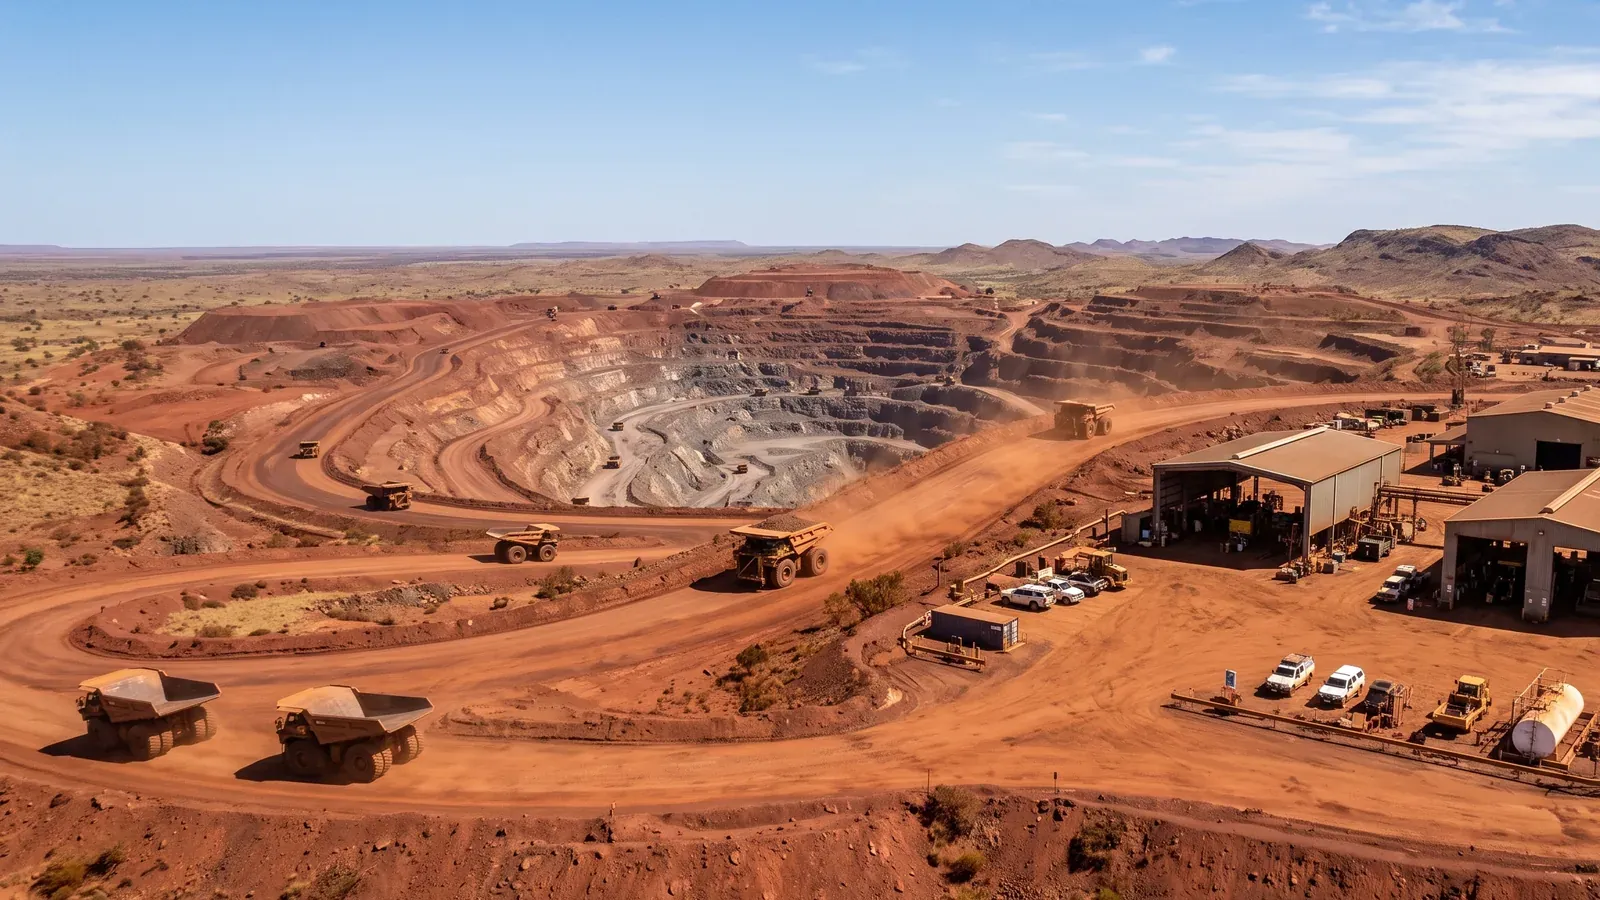
Client: Ross Industries
Industry: Mining procurement and resources
Application: Humidity control in remote mining infrastructure
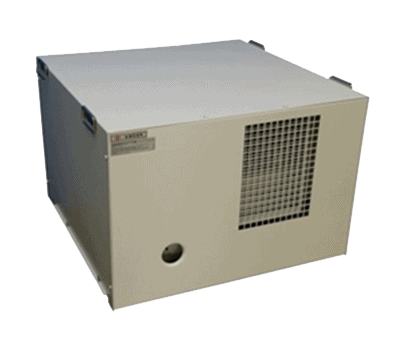
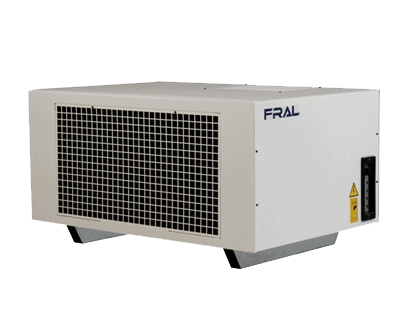
Solution: Ongoing supply of commercial and industrial dehumidifiers
Location: Western Australia
Projects: Barrow Island, Wheatstone and Tier 1 mine sites
Ross Industries is a Western Australian procurement specialist supporting Tier 1 operators across mining and energy, including Chevron and BHP.
They source equipment for critical infrastructure, where reliability, compliance and delivery certainty are weighted well above unit price.
Results at a Glance
- 3 major projects: Barrow Island, Wheatstone and Tier 1 mine sites
- Tier 1 operators supplied through one procurement partner
- Repeat engagement across multiple years
The Challenge
Western Australian mining sites are among the hardest operating environments in the country.
Heat, humidity, dust and long distances from service support all compound each other.
Their clients needed humidity solutions that could:
- Control moisture in accommodation units, mechanical rooms and storage areas
- Protect personnel and equipment in remote, high-risk locations
- Scale across multiple projects and sites without changing specification
- Come with supplier support and delivery that holds to a project schedule
For a procurement firm, supplier reliability is the product. A late or non-performing unit becomes their problem, not the manufacturer's.
Our Solution
Moisture Cure has supported Ross Industries across several major initiatives, supplying commercial and industrial grade dehumidifiers.
Projects supported include:
- The Barrow Island LNG project
- Chevron's Wheatstone project
- Multiple Tier 1 mine sites across Western Australia
Equipment was selected for:
- Durability in extreme, remote-site conditions
- Consistent year-round performance under continuous load
- Proven moisture protection across both infrastructure and living quarters
Ross Industries now refers Moisture Cure as a standing procurement option for humidity control.
Results and Impact
Reported outcomes:
- Reliable performance across high-value Western Australian projects
- Procurement confidence carried through to major energy and mining end clients
- Repeat engagement across multiple projects and years
- Long-term operational performance in the field
What Procurement Teams Need From a Supplier
For a procurement specialist, the equipment is only part of what is being bought.
The requirements that decide who gets the order:
- Stock certainty. A confirmed quantity available now, not a lead time that moves
- Specification stability. The same model available across a multi-year project, so sites do not diverge
- Sizing support. Technical advice at quoting stage, before the end client commits
- Delivery to site. Freight into remote locations handled rather than handed back
- Accountability. A supplier who answers the phone when a unit fails 1,200 kilometres from the nearest branch
Repeat engagement across multiple projects is the only real evidence that a supplier meets all five.
Related Solutions
- mining equipment storage humidity protection. Corrosion in equipment stores is the highest-cost moisture failure on a mine site.
- power plant humidity regulation. Plant rooms on resources sites carry a comparable continuous-duty requirement.
- industrial dehumidifiers. The industrial range covers the airflow volumes these sites require.
Procurement Support for Resources Projects
Procurement teams need sizing advice, stock certainty and a specification that holds across sites.
Contact Moisture Cure Commercial to discuss project supply, staged delivery and site trials.
Contact Moisture Cure Commercial for expert sizing advice on your application.